Manufacturing & quality
Precision-engineered every step of the way
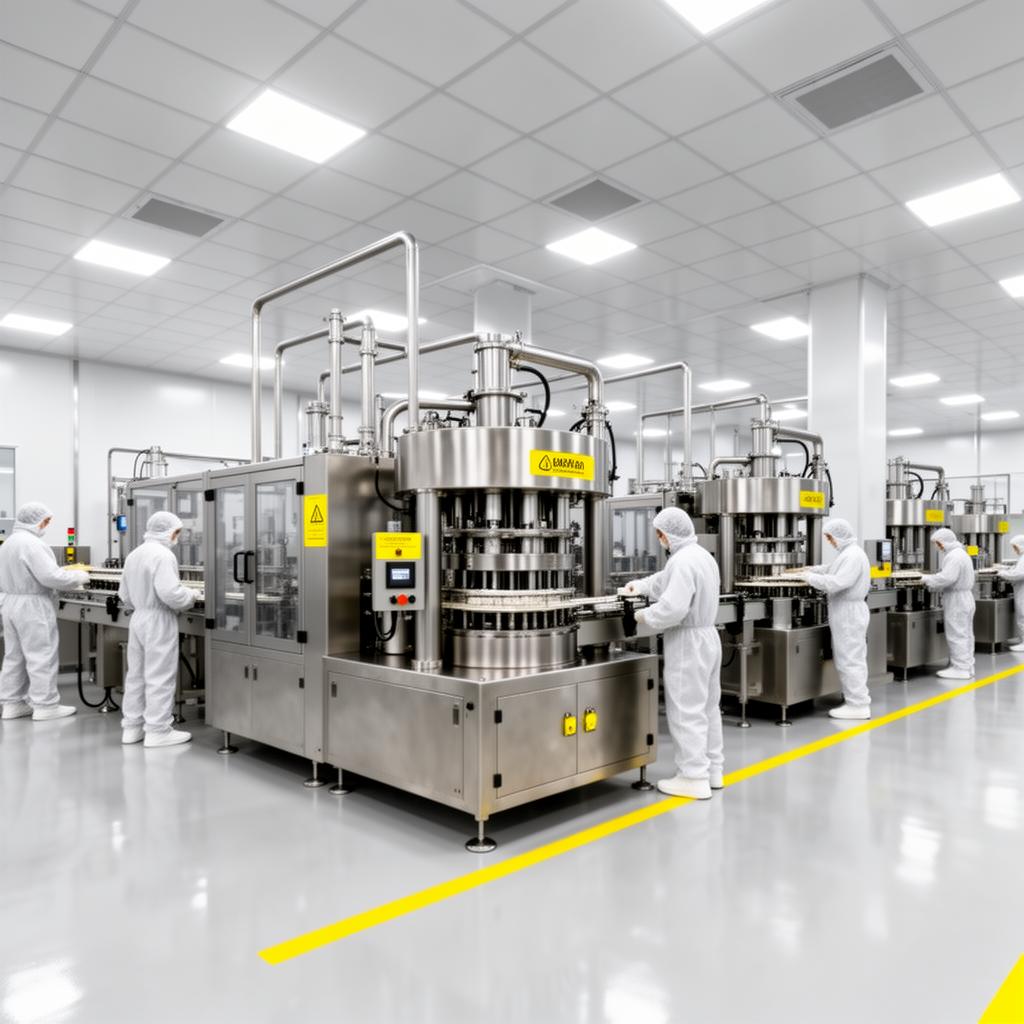
Our facility is built around globally accepted GMP principles, advanced equipment and an uncompromising QA culture.
Process
From raw material to release
01
Raw Material Intake
Vendor-qualified APIs and excipients undergo identity and purity testing.
02
Formulation
Validated processes blend, granulate and compress under controlled conditions.
03
Production
Automated tablet, capsule, liquid and parenteral lines.
04
In-process QC
Hardness, friability, weight and assay checks at every stage.
05
Release Testing
Finished-product analysis and stability data before dispatch.
06
Packaging & Dispatch
Tamper-evident packaging with full batch traceability.
Quality control
A culture built around zero compromise
Our QC laboratory is equipped with HPLC, UV spectrophotometry, dissolution apparatus and microbiology testing capabilities. Every batch is analysed, documented and approved by qualified pharmacists before release.
- ICH-compliant stability chambers
- Validated cleaning and sterilisation procedures
- Digital batch records & full traceability
- Annual third-party audit programme
Certifications
Compliance standards we meet
WHO-GMP
ISO 9001:2015
ISO 14001
Halal Certified
DRAP Approved
PIC/S Aligned